Last updated: November 02, 2026
Generating accurate G-code from Mastercam for Fanuc CNC controllers requires a data translator properly configured for your specific machine hardware. Utilizing an optimized mastercam fanuc post processor ensures seamless translation of CAM toolpaths into safe, precise CNC commands—preventing axis collisions and significantly reducing cycle times on the shop floor.
In modern manufacturing, acquiring a CAM software license is only the first step. The true foundation of a successful machining operation lies in post-processing. A custom-tailored post processor delivers smooth machine motion, eliminates jerkiness, and prevents unexpected machine stops or syntax errors when loading programs into the Fanuc controller.
Understanding the Role of Mastercam Fanuc CNC Post Processors
A mastercam fanuc post processor is a specialized configuration file inside Mastercam that translates raw toolpath data (NCI) into standard G-code and M-code syntax fully compatible with Fanuc CNC controllers—such as Fanuc 0i-MF, 31i-B, 18i-MB, or 5-axis Series 30i controls.
In professional CAM programming, every CNC control system uses distinct syntax, canned cycles, and coordinate system handshakes. Fanuc controllers are globally renowned for their stability, yet they demand strict syntax structure—including G43 H tool length offsets, G54–G59 work offsets, and G05.1 Q1 / G05 P10000 High-Speed Machining (AICC/AIAPC) modes. A properly developed post processor bridges the software-hardware gap to ensure every move executes flawlessly without triggering control alarms or hardware damage.
Many programmers utilizing Mastercam Milling solutions encounter issues where Mastercam Verify shows no collisions, yet the machine crashes, or the Fanuc controller throws syntax alarms (such as PS0010 or PS0007), executes sudden retracts, or ignores coolant codes. These issues stem directly from using generic post processors not tailored to the specific machine build.
Furthermore, for job shops serving global OEMs, standardized post-processing ensures consistent surface finish, tighter tolerances, and eliminates the need for manual G-code editing at the machine control panel.
Architecture of a Mastercam Post Processor (.PST) File
Behind Mastercam’s user interface lies the MP (Mastercam Post) language architecture. A post processor is not merely a text template; it is an executable script engine that parses intermediate binary NCI data generated by Mastercam toolpaths and formats it line-by-line into ISO G-code.
1. Core Entry Blocks (psof$, ptlchg$, peof$)
The execution flow of an MP script relies on predefined entry points called post blocks:
psof$(Start of File): Executes when writing the header of the G-code program. It sets up initial safety lines, output units (G20/G21), plane selection (G17/G18/G19), absolute programming mode (G90), work coordinate systems (G54), and initial tool loading.ptlchg$(Tool Change): Triggers whenever a new tool is called in the operation list. It manages spindle retracts, coolant deactivation (M09), automatic tool changer (ATC) positioning moves (G91 G28 Z0.), tool pre-staging, and application of new length offsets (G43 Hxx).peof$(End of File): Executes at the conclusion of the posting process. It ensures all axes return safely to reference home positions, stops the spindle (M05), turns off coolant, and appends the program end code (M30 or M02).
2. Variable Declarations and Logic Switches
Inside a custom .pst file, post developers utilize specific switches to control modal G-code outputs. For instance, setting force_wcs : 1 ensures that G54 is explicitly re-stated after every tool change, preventing downstream indexing errors. Variable parameters also control whether sequence numbers (N-lines) are output on every block or restricted only to tool change callouts, preserving controller memory.
Fanuc Controller Series & Specific Syntax Requirements
Fanuc controls share a core ISO G-code structure, but different controller generations and machine tool builder (OEM) integrations introduce subtle syntax variations. Tailoring a mastercam fanuc post processor requires accounting for these hardware-specific nuances.
1. Fanuc Series 0i (0i-MD, 0i-MF, 0i-TF)
The 0i series represents the most widely deployed CNC control family for 3-axis mills and 2-axis lathes. While highly reliable, memory capacity on older 0i-MD units can be constrained. An optimized post processor for Fanuc 0i controls strips redundant trailing zeros, formats canned cycles efficiently (G81, G83, G73), and ensures rigid tapping utilizes M29 prior to the G84 cycle call.
2. Fanuc Series 16i / 18i / 21i
These legacy controls are standard across many high-precision Japanese and Taiwanese machining centers. They frequently feature extended work offsets (G54.1 P1 through P48). The post processor must be configured to format extended offsets dynamically based on Mastercam’s WCS fixture numbers, converting WCS 6+ into G54.1 Px blocks automatically.
3. Fanuc Series 30i / 31i / 32i Model B
Engineered for high-speed mold making and multi-axis complex machining, the 31i and 30i series support advanced look-ahead algorithms, dynamic vector adjustments, and multi-channel synchronization. Post processors for these controls must manage high-speed smoothing modes seamlessly without triggering control alarms.
4. OEM Machine Tool Builder Customizations
Machine OEMs (such as Doosan/DN Solutions, Fanuc Robodrill, Makino, Akira-Seiki, or Kitamura) add custom ladder logic and M-codes to Fanuc hardware. For example, triggering chip conveyors, high-pressure through-spindle coolant (TSC), air blast, or automatic door operations requires post processors customized with OEM-specific M-codes (e.g., M08 for flood coolant vs. M131 for 70-bar TSC).
Risks of Using Unoptimized Generic Post Processors
Fanuc CNC controls power the majority of machining centers worldwide. However, relying on default post processors (Generic Fanuc) across various 3-axis to 5-axis machine tools introduces significant technical risks:
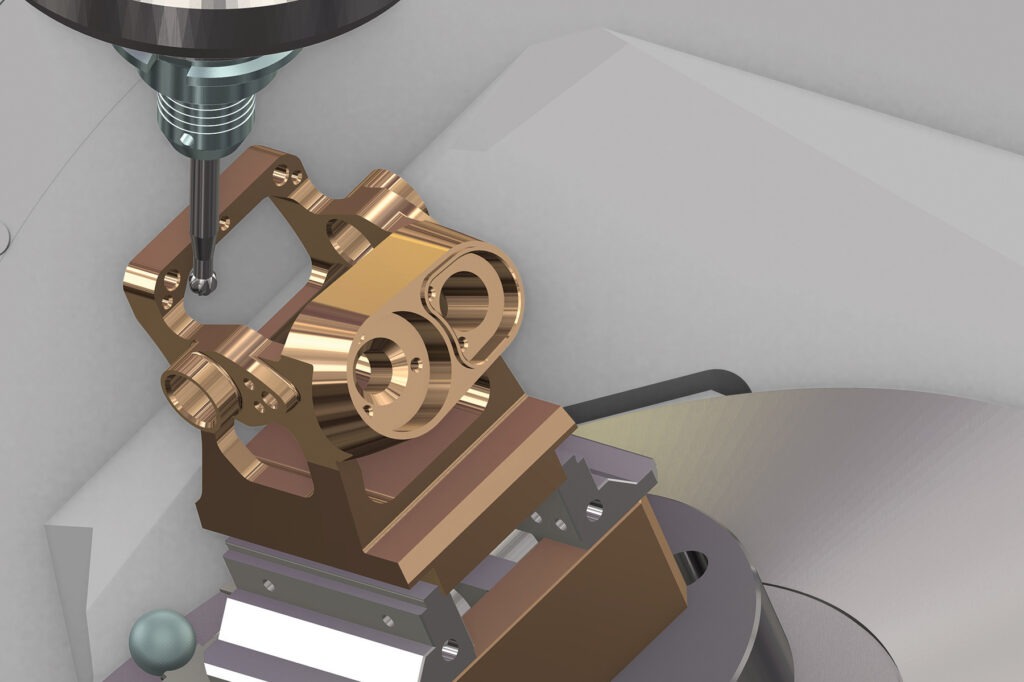
- Axis Collisions and Tool Breakage: Incorrect tool retraction formatting, missing safe Z-retract commands (G91 G28 Z0.) before X/Y movements, or missing G49 tool length cancel codes during automatic tool changes (ATC) can lead to catastrophic crashes at full rapid speeds.
- Work Offset Misalignment: Incorrect handling of extended work coordinate systems (G54.1 P1 to P48) in complex multi-fixture setups can cause off-center machining or cutter gouging into workholding equipment.
- Inability to Activate High-Speed Mold Machining: Modern Fanuc controls rely on look-ahead algorithms to smooth out high-speed toolpaths. If the post processor fails to output G05.1 Q1 (or G05 P10000) at toolpath entry and G05.1 Q0 at exit, the machine will stutter, vibrate, and leave noticeable feed marks on surface finishes.
- Wasted Cycle Time: Unnecessary redundant blocks, improper canned cycle formatting (G81/G83), and inefficient retract moves extend program runtime and degrade shop productivity.
- Specialized Cycle Syntax Errors: Specialized operations like rigid tapping (M29) or boring cycles will snap cutting tools inside threaded holes if not explicitly defined within the post processor script.
According to Fanuc CNC system specifications, controllers from entry-level Fanuc 0i-Mate to high-end 31i Model B systems utilize specific M-codes customized by machine tool builders. Optimizing your post processor is therefore mandatory prior to volume production.
High-Speed Machining (HSM) & Look-Ahead Control Configuration
High-speed surface milling (3D Dynamic Motion and high-feed trochoidal milling) creates thousands of short line segments per second. Without look-ahead acceleration/deceleration control, Fanuc machine tools experience extreme mechanical vibration, tool chatter, and buffer underflow.
1. AI Contour Control (AICC / AICC II) – G05.1 Q1
Fanuc’s Advanced Integrated Contour Control evaluates upcoming G-code blocks in real time to adjust feed rates dynamically around sharp corners and tight radii. To implement AICC via Mastercam:
- The post processor reads the tolerance and toolpath smoothing settings from Mastercam’s Miscellaneous Values (Misc Ops).
- Upon entering high-speed roughing or finishing toolpaths, the post automatically inserts
G05.1 Q1 R1(where R1 to R10 denotes accuracy level vs. speed preference). - Upon toolpath completion, the post outputs
G05.1 Q0to deactivate AICC prior to tool retracts.
2. High-Speed Cycle (AIAPC) – G05 P10000
On high-end Fanuc controls (such as 31i-MB), High-Speed Arbitrary Velocity Control utilizes the G05 P10000 syntax block. Deactivation requires G05 P0. A correctly authored mastercam fanuc post processor handles logic switching between G05.1 and G05 P10000 automatically based on selected controller parameters.
3. Look-Ahead Activation via G08 P1
For legacy Fanuc 16i/18i controls equipped with HPCC (High-Precision Contour Control), look-ahead is toggled using G08 P1 before cutting moves and disabled via G08 P0 after retracts. Integrating G08 mode directly into post processor tool change blocks eliminates the risk of operators forgetting manual edits.
Code Comparison: Default Generic vs. Customized Fanuc Post Output
Comparing actual G-code blocks illustrates the technical differences between default output and an optimized post processor engineered by authorized specialists:
Unoptimized Generic Post Output (High Crash Risk & Slow Execution)
%
O0001 (PART_TOP_PLATE)
N100 G20 G00 G17 G40 G49 G80 G90
N102 T1 M06
N104 G00 G90 G54 X1.25 Y-2.35 S3500 M03
N106 G43 H1 Z1. M08
N108 Z.1
N110 G01 Z-.5 F25.
N112 X3.5 F45.
... (10,000 lines of un-smoothed code)
N950 Z1.
N952 M05
N954 M09
N956 G28 X0 Y0 Z0 (DANGER: Non-standard retract move!)
N958 M30
%
Customized Fanuc Post Output (100% Safe, Automated HSM & Clean Syntax)
%
O1001 (PART_TOP_PLATE_REV3)
(PROGRAM NAME - TOP_PLATE)
(DATE/TIME  - 02-NOV-2026)
(TOOL - 1 | 12MM 3-FLUTE CARBIDE ENDMILL | H1 | D1)
G00 G17 G20 G40 G49 G80 G90
G91 G28 Z0.
T01 M06
(OPERATION 1: DYNAMIC MILL ROUGHING)
G00 G90 G54 X1.25 Y-2.35 S6500 M03
G43 H01 Z1.0 M08
G05.1 Q1 R3 (ACTIVATE FANUC AICC II HSM SMOOTHING)
Z0.1
G01 Z-0.5 F35.0
X3.5 F120.0
...
G05.1 Q0 (DEACTIVATE FANUC AICC II)
G00 Z1.0 M09
M05
G91 G28 Z0.
G28 Y0. (SAFE TABLE PRESENTATION TO OPERATOR)
M01
T02 M06 (PRE-STAGED NEXT TOOL)
M30
%
4 Steps to Export Accurate G-Code for Fanuc CNC Machines in Mastercam
To guarantee safe, efficient G-code output for Fanuc CNC machines, CAM programmers should adhere to this 4-step workflow:
Step 1: Select the Correct Machine Definition and Control Definition
Within Mastercam Mill, navigate to the Machine tab and select your machine type. Ensure you load the specific .mcam-control and .mcam-mmd files provided for your specific Fanuc machine model, rather than generic default definitions.
Step 2: Verify Post Processor Settings in Toolpath Manager
Before clicking Post (G1), open the Files section in the Toolpath Group manager to confirm that the linked .pst file matches your verified post processor. Confirm program number formats (Oxxxx), program names, and Work Coordinate System (WCS) settings align with physical machine setups.
Step 3: Simulate and Verify Toolpaths (Verify & Backplot)
Run a full simulation using Mastercam’s Backplot and Verify tools. Check tool assembly lengths, holder clearance against fixtures, and transition moves between roughing (Dynamic Motion) and finishing operations. Catching motion errors digitally prevents expensive shop-floor crashes.
Step 4: Post Output and Validate G-Code Syntax
Click Post Selected Operations (G1). The G-code file will open automatically in Mastercam Code Expert. Perform a quick manual audit on critical blocks:
- Header block: Ensure safety blocks like
G00 G17 G21 G40 G49 G80 G90are present. - Tool Change block: Verify
Txx M06, spindle startSxxxx M03, safe Z approach, and length offset calloutsG43 Hxx Zxx M08. - Footer block: Confirm coolant off
M09, spindle stopM05, home returnG91 G28 Z0., and program endM30.
Comparison: Generic vs. Customized Mastercam Fanuc Post Processor
The table below highlights technical differences between using standard default post files versus a customized post processor tailored by authorized technical experts:
| Comparison Criteria | Generic Fanuc Post Processor | Customized Fanuc Post Processor (Solid & Soft) |
|---|---|---|
| Operational Safety | Moderate crash risk due to generic retract routines. | 100% safe, pre-configured retract clearance points and axis locks. |
| High-Speed Machining (AICC/AIAPC) | Requires manual editing to insert G05.1 Q1 / G05 P10000 blocks. | Automated G05.1 / G05 output triggered by Mastercam toolpath parameters. |
| Multi-Axis Support (4-Axis / 5-Axis) | Prone to rotary interpolation errors; lacks native G68.2 TWP support. | Full integration of G68.2 (TWP), Dynamic Fixture Offset, and RTCP (G43.4/G43.5). |
| Custom OEM M-Codes | Limited to basic M-codes (M03, M04, M05, M08, M09). | Supports OEM custom M-codes (fixture clamp/unclamp, air blast, chip conveyor). |
| Setup Time at Machine | Requires manual code tweaking by operators at the controller. | Direct drip-feed/DNC execution with zero manual code modifications. |
For manufacturing enterprises delivering precision parts to global supply chains, standardizing code output with a dedicated post processor is vital to optimizing cycle efficiency and protecting high-capital CNC assets.
Advanced Configurations for 4-Axis and 5-Axis Fanuc Controllers
Programming 4-axis and 5-axis Fanuc CNC machinery requires advanced post processors capable of handling complex kinematic transformations. When accessing the official Mastercam Post Processor library, ensure these advanced options are enabled:
1. Tilted Working Plane (G68.2) for 3+2 Axis Machining
The G68.2 command enables Fanuc controls to define tilted coordinate systems without requiring programmers to manually recalculate origin offsets. A custom post processor automatically computes Euler angles (I, J, K) or roll-pitch-yaw angles (X, Y, Z), outputting accurate G68.2 X.. Y.. Z.. I.. J.. K.. blocks for simple 5-axis fixture alignment. Unwinding coordinates is automatically handled via G69.
2. Tool Center Point Control (TCP / G43.4) for Simultaneous 5-Axis Machining
During continuous 5-axis motion, tool vectors and rotary axes move simultaneously. Command G43.4 (or G43.5) instructs the Fanuc control to compute dynamic tool length compensation in real-time based on rotary pivot positions (A, B, C). A robust 5-axis post processor manages smooth entry and exit transitions for G43.4 to prevent tool gouging when switching between 3-axis and 5-axis toolpaths.
3. Rotary Axis Limit Management (Axis Limit Control)
Advanced post processors actively monitor machine physical envelope limits, automatically triggering rewind moves or alternate angle solutions when a rotary table approaches physical travel limits (e.g., C-axis exceeding +/- 360 degrees or A-axis tilting beyond -110 degrees), preventing unexpected mid-cut mid-program stops.
Troubleshooting Common Fanuc Controller Syntax Alarms
When G-code is generated using generic or misconfigured post files, Fanuc controllers display specific alarm codes. Understanding these alarms helps pinpoint post processor configuration errors:
- PS0003 (TOO MANY DIGITS): Occurs when address values exceed controller register formats (e.g., outputting 4 decimal places on a control set up for 3 places). Fixed by adjusting post format statements (
fmtlines). - PS0007 (ILLEGAL USE OF DECIMAL POINT): Triggered when decimal points are added to integer addresses like G-codes, M-codes, or T-codes (e.g.,
G01.orM06.). Post processor variable formatting must restrict decimals on integer types. - PS0010 (IMPROPER G-CODE): Indicates the controller does not support a posted G-code command (such as calling
G68.2on a control without 3D Coordinate Conversion options installed). - PS0011 (NO FEEDRATE COMMANDED): Occurs when linear interpolation moves (
G01) execute without an active feed rate callout. The post must enforce modal feed rate outputs (force_f) after tool positioning moves. - SR0590 (TOOL LENGTH OFFSET NOT FOUND): Triggered when
G43is commanded without a validHoffset callout, or when theHindex does not exist in the offsets memory table.
Custom Mastercam Fanuc Post Processor Services from Solid & Soft
Modifying Mastercam post processor files (using Mastercam’s MP scripting language) demands deep expertise in both software architecture and hands-on CNC machining mechanics. To eliminate code errors and guarantee machining safety, Solid & Soft—an official authorized Mastercam reseller—provides comprehensive post processor customization services for all Fanuc-driven machine tools.
Solid & Soft’s application engineering team performs on-site machine audits, analyzes control parameter structures, and builds custom post files matched to your exact shop floor configuration. Mastercam license holders backed by Solid & Soft benefit from dedicated technical support, integrated Mastercam Probing automated inspection routines, on-machine test cutting, and comprehensive training.
Contact Solid & Soft today to upgrade your mastercam fanuc post processor setup and maximize your CNC machine tool efficiency.