
Last updated: 20/08/2026
Mastercam Dynamic Milling is a revolutionary high-speed machining strategy that uses intelligent algorithms to maintain a constant tool engagement angle and uniform cutting forces throughout the entire process. For mechanical engineers and CNC programmers aiming to maximize productivity, implementing Mastercam Dynamic Milling helps optimize cutting tool lifespan, increase spindle speeds, and significantly reduce roughing time for complex components across various industrial sectors.
Understanding Mastercam Dynamic Milling Technology
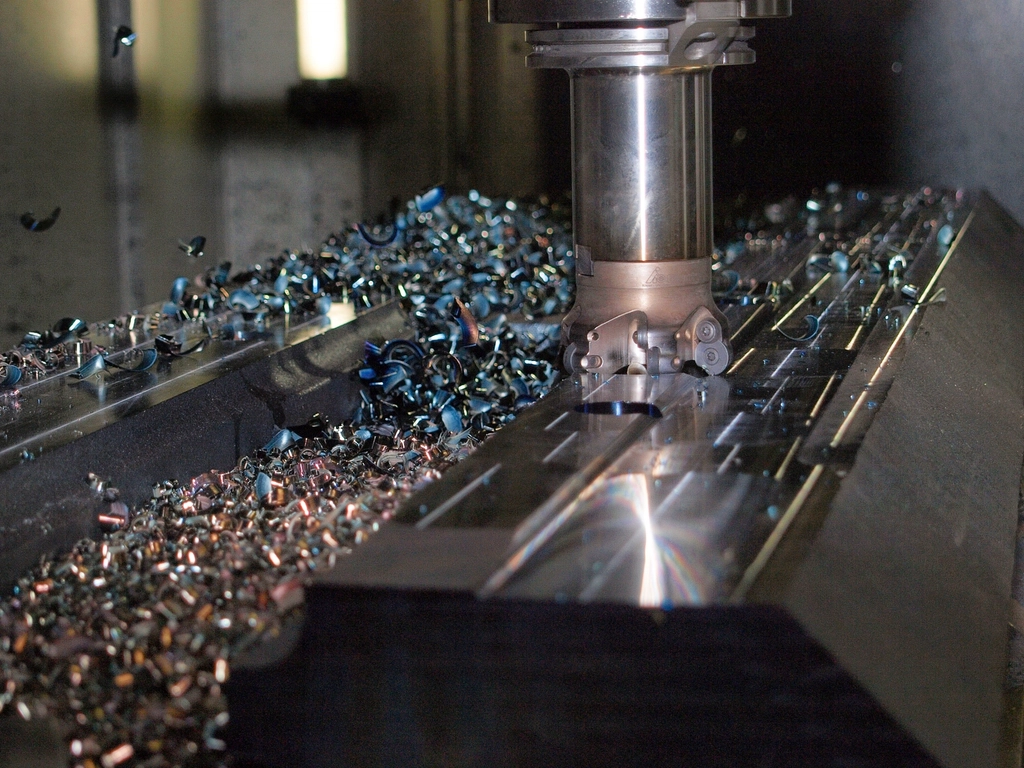
Dynamic Milling is an advanced roughing toolpath developed exclusively and integrated directly into the Mastercam software. Unlike traditional milling, which features constantly changing tool engagement angles and sudden load spikes in corners, Mastercam Dynamic Milling automatically calculates smooth trochoidal or spiral trajectories. As a result, excess material is removed with consistent chip thickness, allowing CNC machines and cutting tools to operate stably at high intensities.
In modern manufacturing environments, efficiency is the primary metric for success. Shop floors are constantly pressured to deliver parts faster, with tighter tolerances, and at a lower cost per component. Traditional roughing strategies often fall short because they fail to utilize the full potential of modern CNC machines and cutting tools. By keeping the cutter engaged uniformly, Mastercam Dynamic Milling addresses these inefficiencies directly, transforming how roughing operations are executed in aerospace, automotive, medical, and general mold-making industries.
Outstanding Benefits of Mastercam Dynamic Milling
 .
Dynamic Milling delivers numerous direct economic and technical benefits to CNC machining workshops by fully unlocking the capabilities of modern machinery. Core advantages include:
- Reduced Tool Wear: Thanks to evenly distributed cutting forces without sudden thermal shock or overload, generated heat is effectively controlled, extending end mill lifespan by 2 to 5 times.
- Increased Material Removal Rates: Engineers can push spindle speeds and feed rates to very high levels, utilizing the entire flute length rather than just the tool tip.
- Shortened Machining Time: The combination of large axial depth of cut and small radial stepover enables rapid chip evacuation, reducing the total cycle time for every part.
Furthermore, the reduction in tool wear translates directly to lower consumable costs. Cutting tools, especially those made from solid carbide or specialized coatings, represent a significant portion of the operational budget in any CNC facility. By implementing Mastercam Dynamic Milling, workshops can drastically reduce the frequency of tool changes, minimizing machine downtime and increasing overall spindle utilization rates.
Comparing Dynamic Milling and Traditional Milling Strategies
Traditional roughing typically employs straight-line or equidistant offset cutting strategies, leading to localized overloads when the tool enters sharp internal corners (square or tight angles). In these areas, the tool engagement angle can spike from 30 degrees up to 180 degrees, causing tool breakage or chipping if feed rates are not reduced promptly.
Conversely, Mastercam Dynamic Milling completely resolves this issue by automatically smoothing out directional changes and keeping the engagement angle at or below a pre-set safety threshold. CAM programming engineers do not need to manually adjust feed rates at every corner, eliminating human error risks and ensuring absolute safety for the spindle system. For further reading on advanced manufacturing techniques, you can explore our CNC machining best practices guide.
When comparing the two methods visually, traditional paths leave erratic loads on the spindle, which can lead to micro-vibrations, chatter, and poor surface finishes even during roughing passes. Mastercam Dynamic Milling maintains a fluid, predictable motion path that protects the machine tool’s mechanical components, including ball screws, bearings, and the spindle itself, thereby reducing long-term maintenance costs and preserving machine accuracy.
Core Parameters to Configure in Mastercam for Dynamic Milling
To operate Dynamic Milling with maximum efficiency on workshop CNC machines, programmers must master and accurately configure the following technical parameters:
- Stepover: Usually set to a small value (5% to 15% of the tool diameter) to ensure the engagement envelope does not exceed the material’s allowable threshold.
- Tool Diameter: Precisely declare the actual tool dimensions on the machine so the Mastercam algorithm can accurately calculate trajectories and stock allowances.
- Max Cut Depth: Allows utilization of the full cutting length of the tool, typically set deeper than traditional milling because cutting forces are distributed along the flute height.
- Entry/Exit: Configure helix entry or smooth arc lead-ins to prevent the tool from plunging vertically and directly into solid material, which causes breakage.
Fine-tuning these parameters requires an understanding of both the workpiece material properties and the specific characteristics of the cutting tool being utilized. Modern tool manufacturers often provide specific chip load and surface speed recommendations tailored for high-speed machining, which can be directly input into Mastercam’s tool library to achieve optimal results with Mastercam Dynamic Milling.
Practical Applications and Transition Notes for Mastercam Dynamic Milling
Dynamic Milling yields the highest efficiency when machining hard-to-cut, high-hardness materials such as alloy steel, stainless steel, titanium, or when deep pocket milling is required in mold manufacturing. In these scenarios, traditional cutting methods often prove inefficient and costly in tool consumption.
When transitioning from traditional toolpaths to Mastercam Dynamic Milling, engineers and machine operators should keep a few crucial points in mind. Avoid the habit of applying low feed rates based on old experiences; instead, trust the parameters recommended by Mastercam and cutting tool manufacturers. Additionally, ensure the coolant system functions properly to continuously dissipate heat from high-speed cutting zones.
Adopting advanced CAM strategies also requires training the programming and operating staff to trust the software. Operators accustomed to hearing heavy, bogged-down cuts in traditional roughing might feel unnerved by the rapid, high-pitch hum of high-speed machining. However, understanding the science behind Mastercam Dynamic Milling reassures teams that the machine is operating within safe mechanical and thermal limits.
Advanced Optimization Techniques and Best Practices
To get the absolute most out of Mastercam Dynamic Milling, programmers should consider several advanced workflow strategies:
- Stock Model Utilization: Always use Mastercam’s stock model feature to track remaining material across multiple operations. This ensures that the Dynamic Milling toolpath only cuts where material actually exists, eliminating air cuts and reducing total cycle times further.
- Air Cutting Minimization: Configure micro-lifts or smooth retracts when the tool must reposition. This prevents dragging the cutter across finished floors and maintains smooth transitions between cut regions.
- Rigid Workholding: Because Mastercam Dynamic Milling allows for aggressive material removal rates, workpiece stability is paramount. Ensure hydraulic vises, vacuum chucks, or custom fixtures can withstand lateral cutting forces without shifting.
By integrating these practices into daily programming routines, CNC facilities can consistently achieve superior productivity gains, reduced tool expenditures, and immaculate surface finishes that require less secondary finishing work. Mastercam continues to reaffirm its position as a leading CAM programming solution, accompanying mechanical engineers on the journey to optimize precision machining productivity.


